OEM ODM Water Cooled Glycol Chiller Manufacturer, Factory
Wuhan Qiaoxin Refrigeration Equipment Co., Ltd. stands out as a leading OEM and ODM manufacturer of water-cooled glycol chillers, dedicated to providing innovative cooling solutions for a diverse range of industries. With years of expertise in refrigeration technology, we pride ourselves on our commitment to quality, efficiency, and customer satisfaction. Our state-of-the-art manufacturing facilities are equipped with advanced technology enabling us to design and produce high-performance chillers that meet stringent international standards. Whether you are in the food and beverage, chemical, or pharmaceutical sector, our customizable glycol chillers are engineered to optimize your cooling processes, enhance product quality, and reduce operational costs, At Wuhan Qiaoxin, we understand that each client has unique requirements, and our flexible OEM and ODM offerings allow us to tailor our products to your specific needs. Our team of skilled engineers and customer service professionals works closely with you to ensure seamless integration and support throughout the project lifecycle. As a trusted partner in cooling solutions, we emphasize sustainability and energy efficiency, helping global buyers achieve their environmental goals while maintaining peak operational performance. Choose Wuhan Qiaoxin Refrigeration Equipment Co., Ltd. for reliable, high-quality water-cooled glycol chillers that drive your business forward

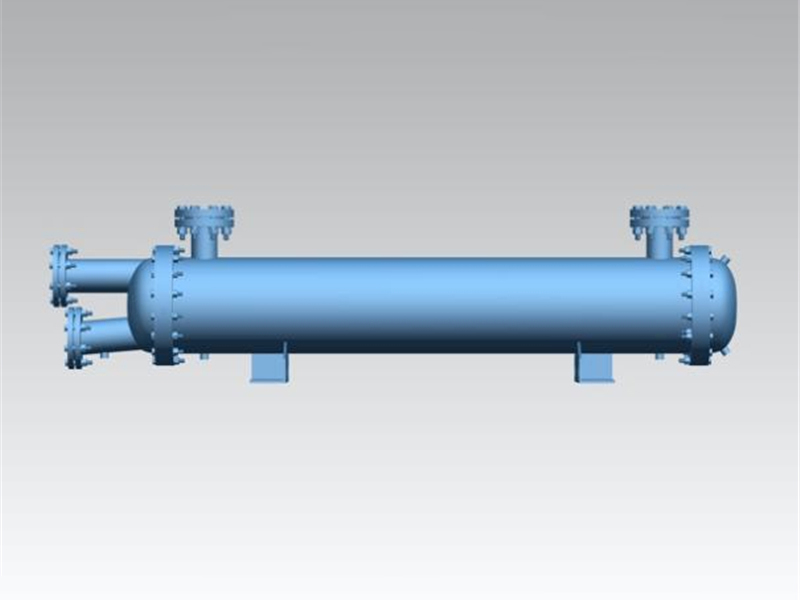
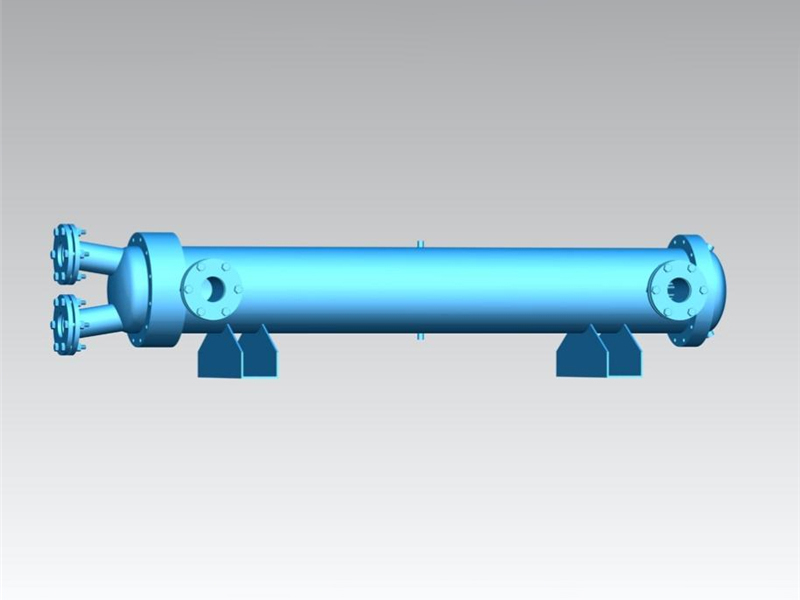
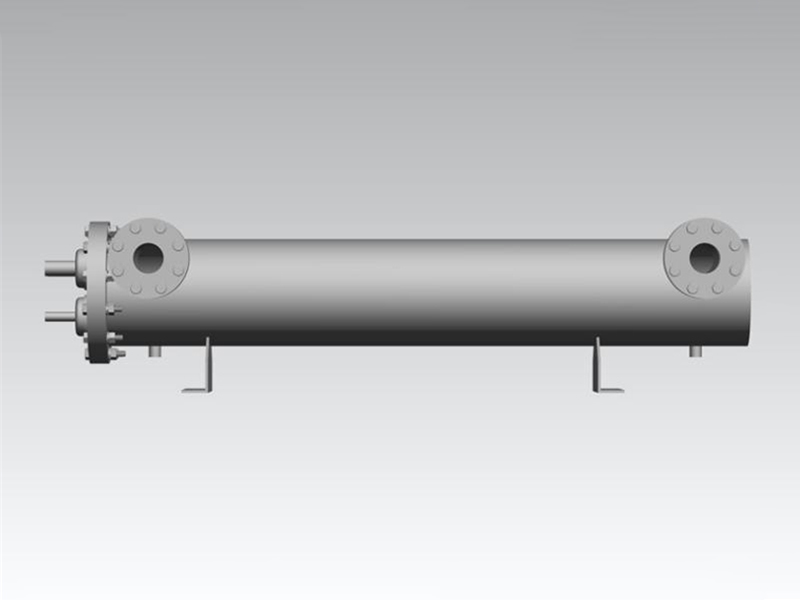
Why China’s Water Cooled Glycol Chiller Trusted by Pros Leads the Global Market
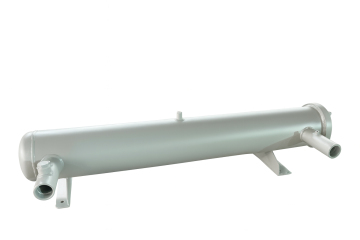
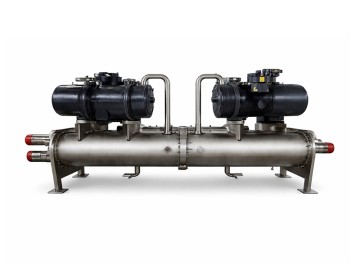
In the evolution of industrial cooling solutions, China’s water cooled glycol chillers have emerged as a trusted choice, widely recognized by professionals across various sectors. With their advanced technology and reliable performance, these chillers not only meet the stringent demands of modern applications but also set the standard for energy efficiency. Their design and manufacturing processes have been fine-tuned over decades, enabling them to provide consistent cooling capabilities while reducing operational costs. This is particularly valuable for industries such as pharmaceuticals, food processing, and HVAC, where precise temperature control is critical.
The success of these chillers lies in their robust construction, innovative features, and ability to operate efficiently under diverse conditions. Integrating shell-and-tube technology enhances their heat exchange efficiency, ultimately leading to improved system performance and reduced downtime. Additionally, their adaptability allows global purchasers to find solutions tailored to their specific needs, making them a go-to option in the competitive international market. The commitment to quality and cutting-edge design ensures that these chillers remain a preferred choice, fostering trust among users and contributing to their dominance in the global landscape.
Why China’s Water Cooled Glycol Chiller Trusted by Pros Leads the Global Market
| Feature | Description | Benefits |
|---|---|---|
| Energy Efficiency | Utilizes advanced technology to minimize energy consumption. | Lower operational costs and reduced carbon footprint. |
| Cooling Capacity | Offers a range from 100 kW to 2000 kW. | Suitable for industrial and commercial applications. |
| Durability | Constructed with high-quality materials for long lifespan. | Reduces maintenance costs and downtime. |
| User-Friendly Control System | Integrated smart controls for easy monitoring. | Enhances operational efficiency and user experience. |
| Compliance | Meets international safety and environmental standards. | Increases market trust and reliability. |
| Versatility | Applicable in various climates and industries. | Flexible solutions for diverse customer needs. |
Top Picks For Water Cooled Glycol Chiller Application Factory
L
Laura Wilson
This was my first time buying from them, and I was pleasantly surprised by the product quality and the dedicated customer service team.
09
January
2026
S
Samantha Rodriguez
I love this product! The quality is fantastic, and the service team was very responsive to my questions.
29
December
2025
J
Jason Bennett
Outstanding quality! The level of customer service provided was exceptional—very responsive and helpful.
24
January
2026
N
Nora White
Superb quality and a remarkable customer service experience. They truly know how to support their clients!
25
January
2026
C
Catherine James
Fantastic quality! Their after-sales team was very professional and genuinely committed to helping.
19
December
2025
S
Steven Robinson
Impressive quality and functionality. The professionalism displayed by the support team made a significant difference.
07
January
2026