Leave Your Message
In the realm of industrial refrigeration, Ammonia (NH3) has long been hailed as the "king of refrigerants." With a Global Warming Potential (GWP) of zero and an Ozone Depletion Potential (ODP) of zero, it stands as the most environmentally sustainable choice for large-scale cooling operations. However, the thermodynamic properties of ammonia require robust, high-precision equipment to manage heat rejection effectively. This is where the Tube in Shell Condenser becomes the heartbeat of the industrial refrigeration plant.
The tube in shell design is engineered to handle the high pressure and corrosive nature of ammonia while maximizing thermal efficiency. Unlike standard commercial HVAC units, industrial ammonia condensers must utilize specialized materials—often carbon steel or high-grade stainless steel—to ensure longevity and safety. The configuration of these condensers allows for massive heat exchange surface areas within a relatively compact footprint, making them ideal for massive cold storage facilities, chemical processing plants, and food production lines.
Constructed with heavy-duty shells and precision-expanded tubes, our condensers are designed to withstand the rigorous demands of 24/7 industrial cycles, resisting vibration and thermal shock.
Advanced baffle designs and optimized tube spacing ensure turbulent flow, which significantly enhances the heat transfer coefficient, reducing energy consumption for the entire plant.
By optimizing the condensation process, these units allow ammonia systems to operate at lower head pressures, directly translating to a smaller carbon footprint and lower utility costs.
Wuhan Qiaoxin Refrigeration Equipment Co., Ltd. was established in 2003 and is located in Wuhan, Hubei Province—China’s major transportation hub connecting nine provinces. The company is a modern enterprise specializing in the research, design, manufacture, and sales of shell-and-tube condensers, evaporators, and other heat-exchange products.
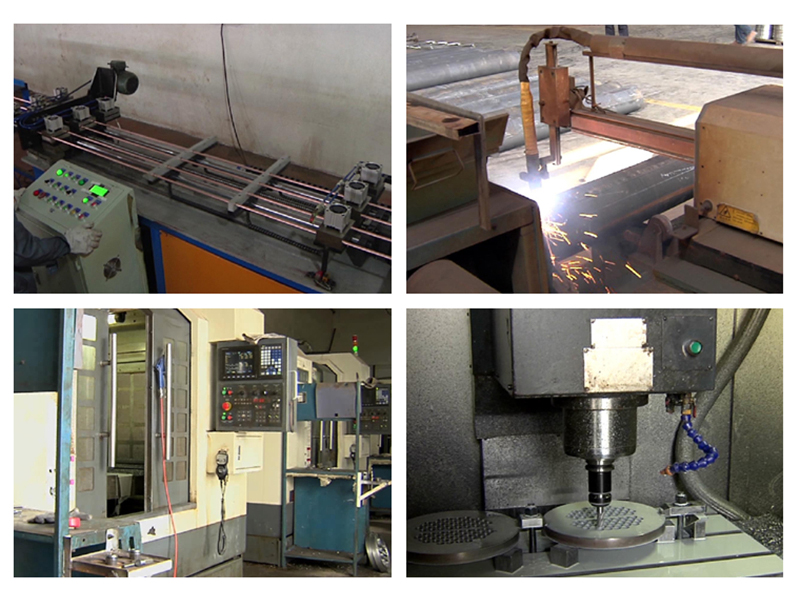
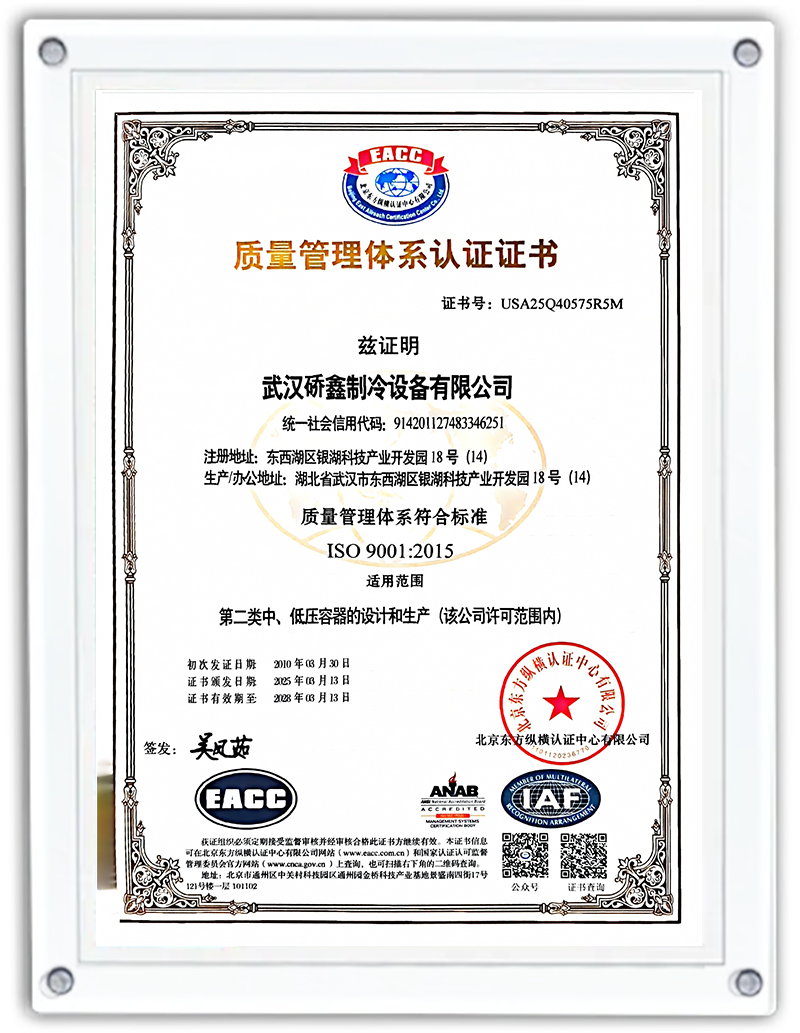
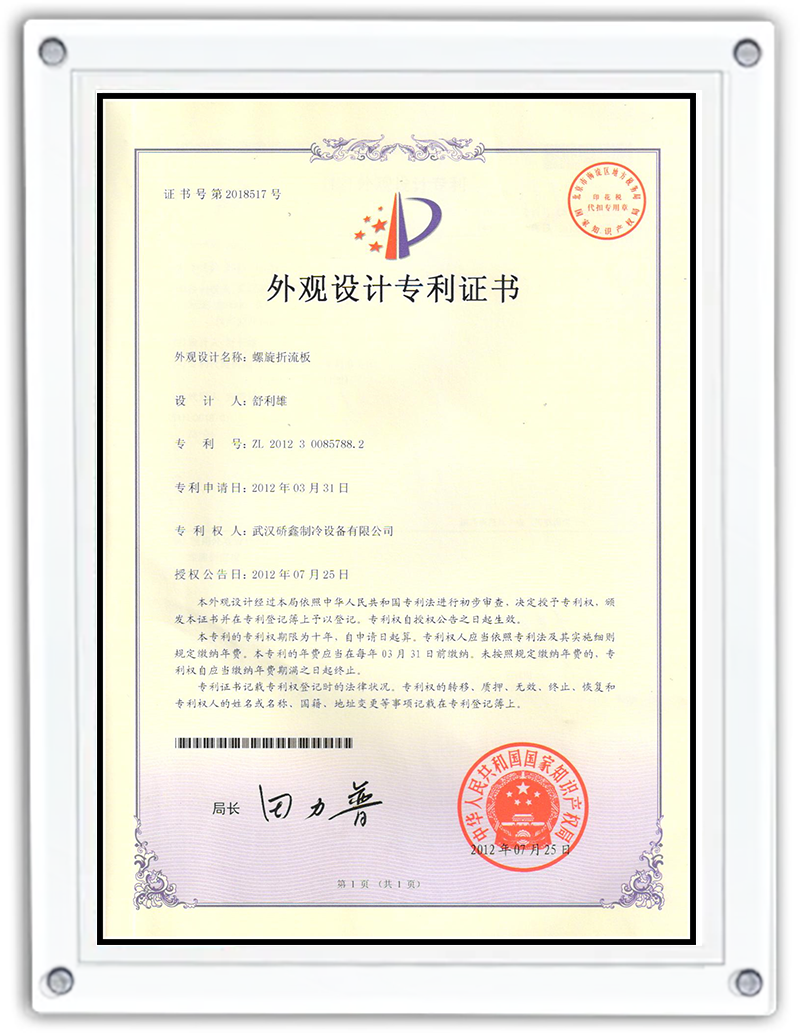
Qiaoxin holds Class I and Class II Pressure Vessel Design Licenses and a Pressure Vessel Manufacturing License. Equipped with CNC machining centers, CNC tube expanders, and CO₂ flux-cored gas-shielded welding equipment, our team delivers precision-engineered solutions for the most demanding global markets.
The global industrial refrigeration market is undergoing a seismic shift. With the tightening of regulations like the Kigali Amendment and the phase-out of HFCs (hydrofluorocarbons), industries are rushing to adopt ammonia-based systems. This has led to a surge in demand for high-performance tube in shell condensers that can operate safely in high-density urban areas or sensitive food processing environments.
One of the most significant trends is the development of "low charge" ammonia systems. Traditionally, ammonia plants required massive amounts of refrigerant, which posed safety risks. Modern shell and tube designs, like those pioneered by Wuhan Qiaoxin, focus on minimizing the internal volume of the condenser while maintaining high heat transfer rates. This allows plants to operate with up to 70% less ammonia, drastically increasing safety without sacrificing performance.
The "AI Tech" revolution is not just for software. Modern condensers are now being integrated with IoT sensors that monitor scaling, pressure drops, and temperature differentials in real-time. Predictive maintenance algorithms can now notify plant managers when a tube cleaning is required before efficiency drops, preventing costly downtime in critical industries like pharmaceutical storage or dairy processing.
In massive distribution centers, maintaining a consistent temperature is non-negotiable. Tube in shell condensers provide the steady heat rejection needed to keep thousands of square meters of freezer space at -25°C. Their ability to handle fluctuating loads makes them superior to air-cooled alternatives in humid or high-temperature climates.
Ammonia refrigeration is vital for controlling exothermic reactions in chemical manufacturing. Our condensers are built to PED (Pressure Equipment Directive) standards, ensuring they can handle the aggressive environments and stringent safety protocols required in the petrochemical sector.
From blast freezing poultry to cooling wort in breweries, ammonia is the preferred choice. The cleanability of the tube side in our shell and tube designs ensures that water-side fouling can be managed easily, maintaining the hygiene and efficiency required in food-grade applications.
QiaoXin was established in Wuhan. Overcoming initial obstacles in product promotion and operational efficiency through professional expertise.
Earned the trust of Midea, one of China’s most well-known enterprises. This partnership remains strong today.
Relocated to current facility and invested in advanced precision machinery and specialized equipment for heat exchanger manufacturing.
Began supplying to international giants including Dunham-Bush and Carrier. Gained broad recognition in both domestic and overseas markets.
Established official export business. Products now reach over 20 countries including South Korea, Malaysia, Vietnam, and India.
Committed to continuous improvement, delivering high-quality products at competitive prices for a sustainable cooling future.
Rigorous testing and international standards compliance.
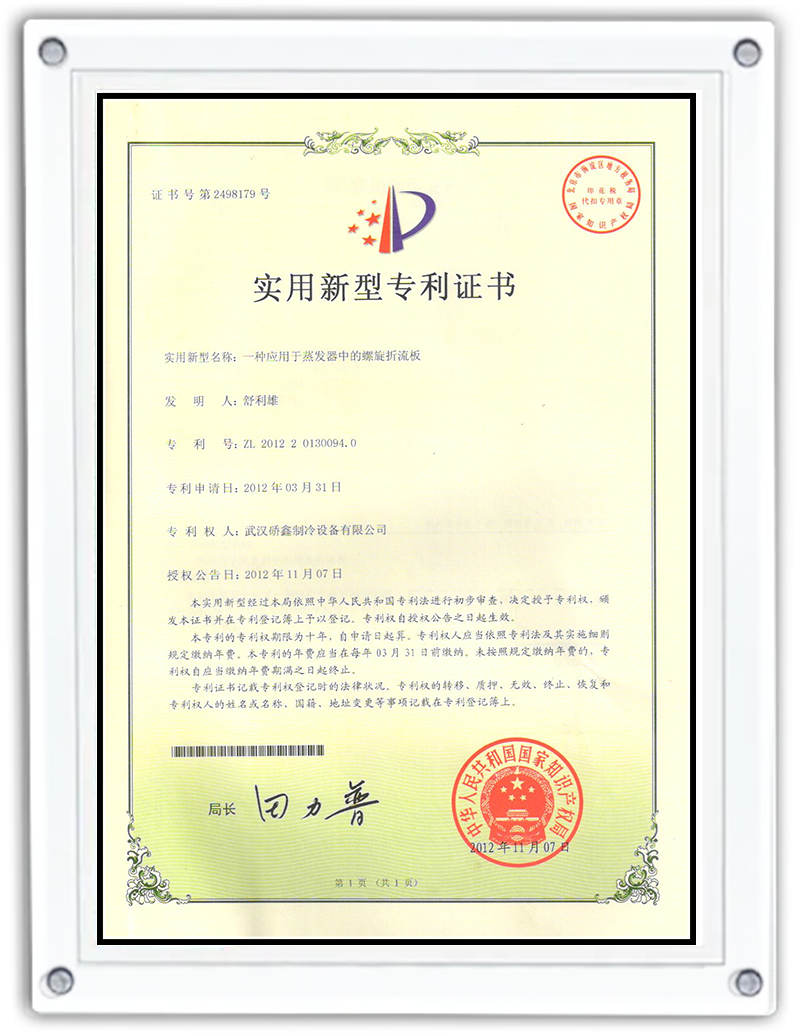
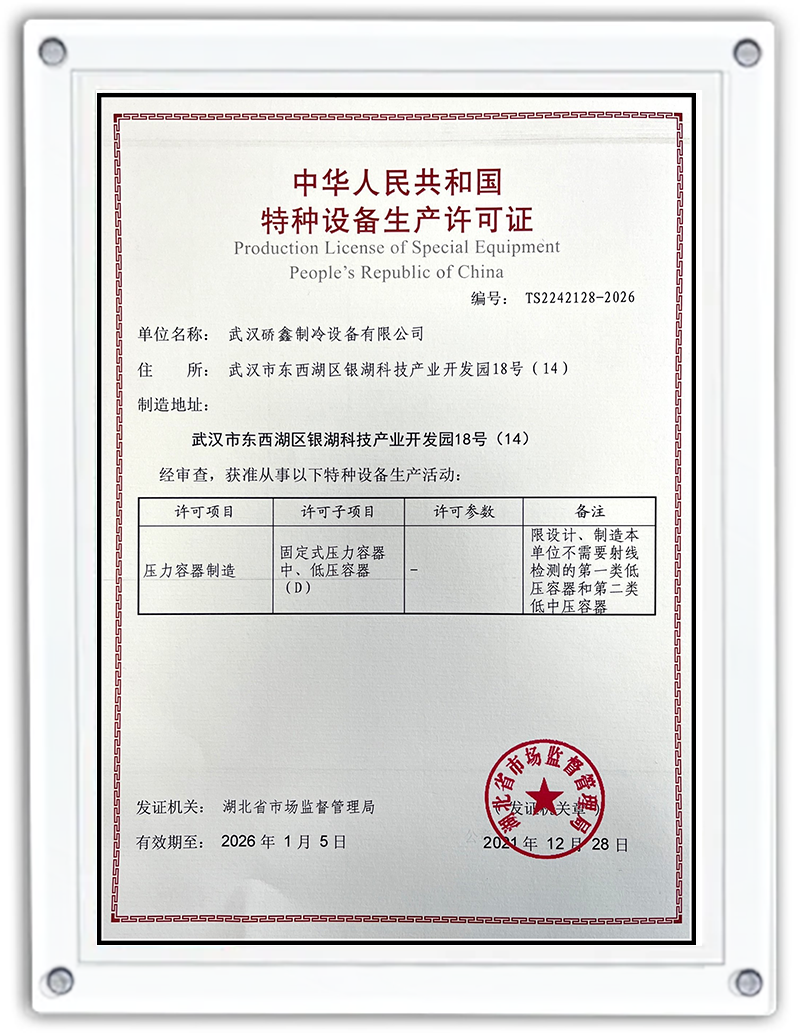
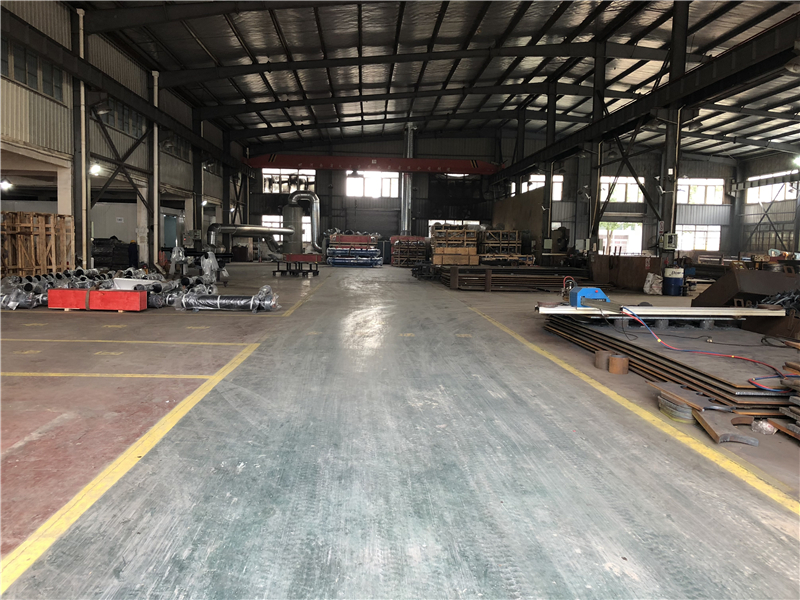
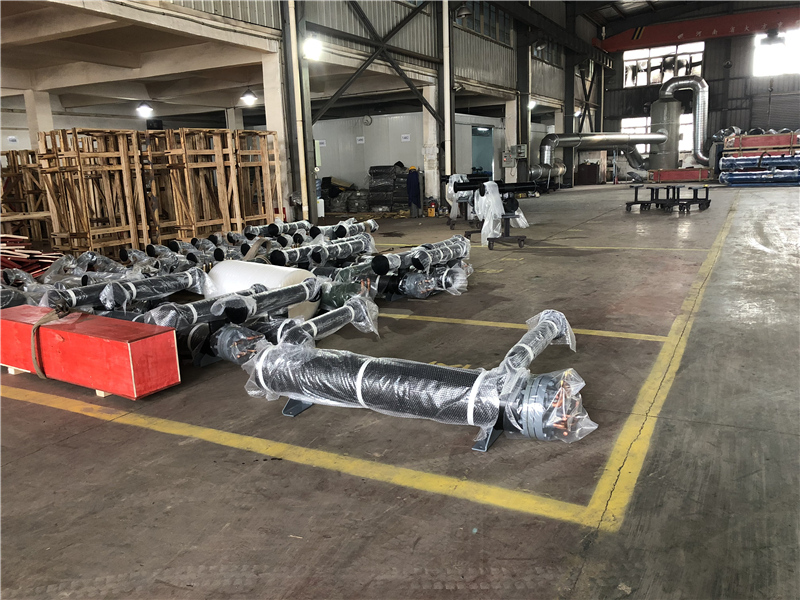
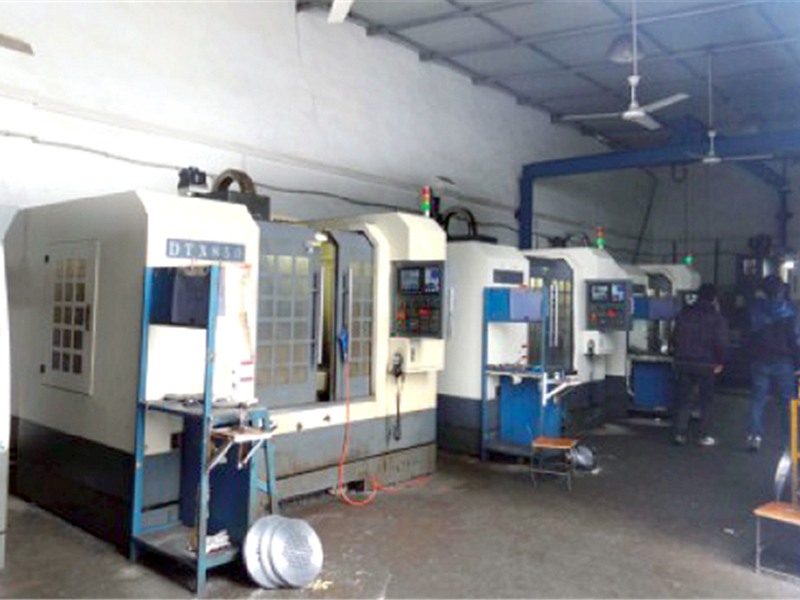
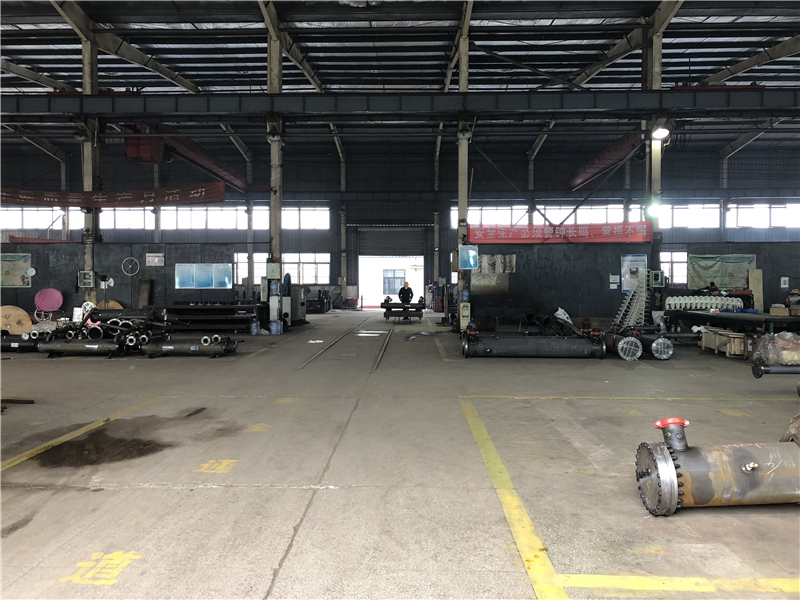
Driven by a strong sense of mission toward the advancement of China’s refrigeration industry, Qiaoxin is committed to applying cutting-edge refrigeration technologies to promote harmonious coexistence between humanity and nature. Looking ahead, the company will continue to follow a path of harmonious, healthy, and scientifically grounded development, upholding the philosophy that “character comes before products, and quality is the lifeblood of an enterprise.” With dedication and enthusiasm, Qiaoxin strives to provide customers with high-value products and reliable, efficient service.
Contact Our Engineering Team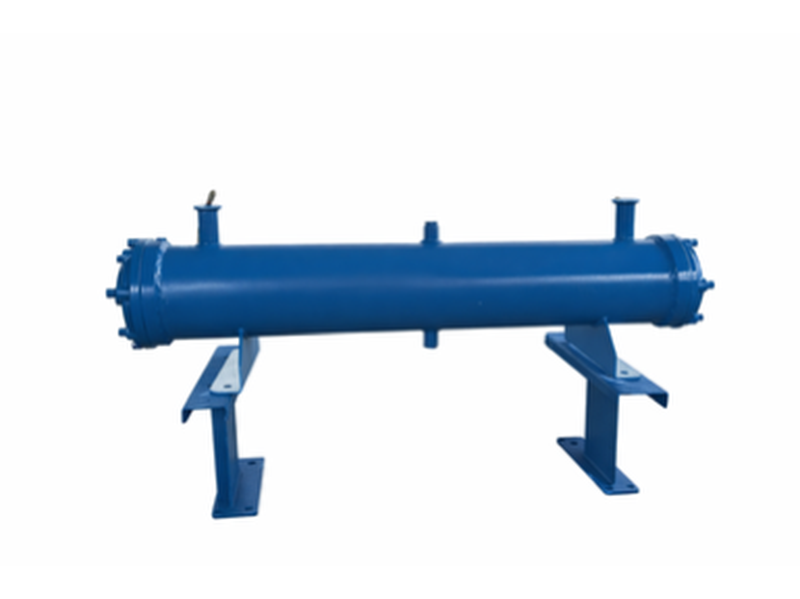 Single-Circuit Condenser for Industrial Ammonia Plants
Reliable Performance Single-Circuit Condenser from China Factory
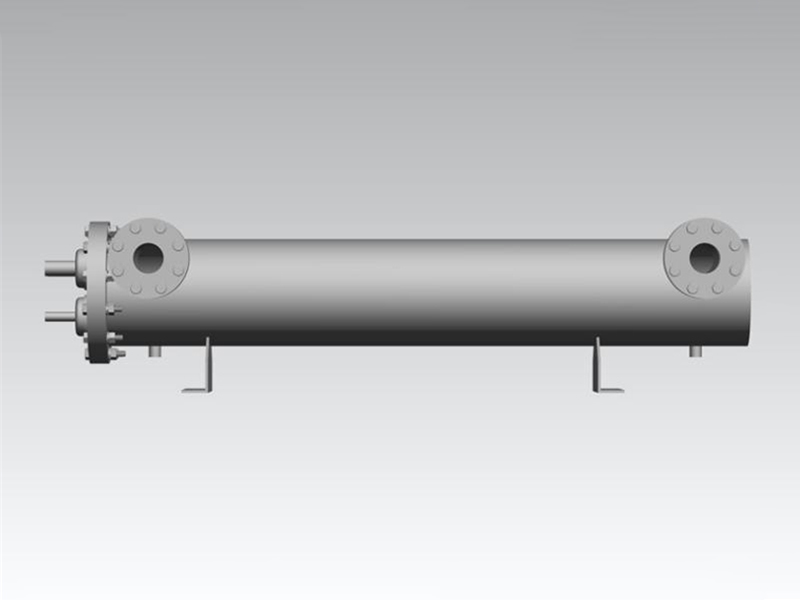 China U-Tube Multi-Pass DX Evaporator for Ammonia Systems
High-Efficiency U-Tube DX Evaporator Suppliers
Reliable Heat Rejection Condenser for Industrial HVAC
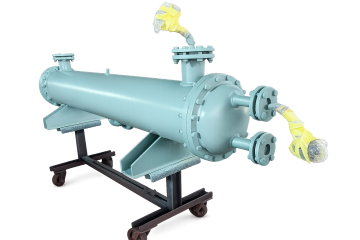 Titanium Tube Steam-to-Water Heat Exchanger for Ammonia Plants
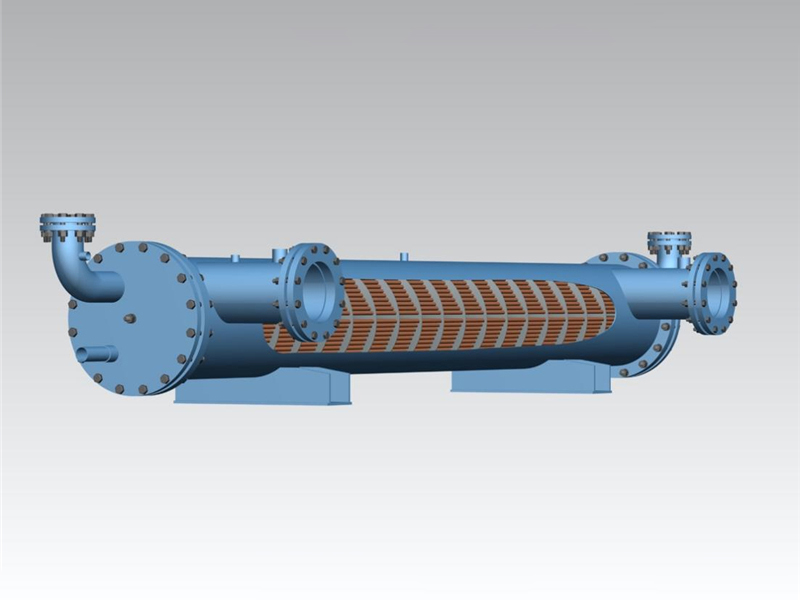 Straight-Tube DX Evaporator with Spiral Baffle Technology
Top Quality Multi-Pass DX U-Tube Evaporator for Industrial Use