Leave Your Message
In the complex and demanding environment of petrochemical refining, maintaining precise thermal management is not merely a matter of operational efficiency — it is a fundamental safety and process integrity requirement. Water cooled condensers, as a core component of industrial refrigeration systems, play an indispensable role in enabling refineries to control temperatures across a wide range of hydrocarbon processing stages, from crude distillation and catalytic cracking to liquefied gas separation and product storage.
Unlike air-cooled alternatives, water cooled condensers deliver significantly higher heat transfer coefficients, making them the preferred choice in high-capacity petrochemical environments where consistent and reliable cooling performance is non-negotiable. As global refining capacity continues to expand and environmental regulations tighten, the demand for advanced, energy-efficient water cooled condenser solutions within petrochemical refrigeration systems has never been greater.
Water cooled condensers in petrochemical refrigeration systems can achieve heat transfer efficiencies up to 40% higher than equivalent air-cooled designs, making them the gold standard for large-scale refinery cooling applications.
The global market for water cooled condensers in industrial refrigeration — particularly within the petrochemical and refining sector — has demonstrated robust growth over the past decade. Driven by expanding refinery capacities across Asia-Pacific, the Middle East, and North America, combined with rising investment in downstream petrochemical processing, the demand for high-performance shell-and-tube and flooded-type condensers has surged considerably.
According to industry analyses, the global industrial refrigeration market is projected to exceed USD 30 billion by 2030, with the petrochemical and chemical processing sector accounting for a significant share of this growth. Water cooled condensers represent a cornerstone technology within this ecosystem, underpinning the cooling infrastructure of refineries that process millions of barrels of crude oil daily.
Key market drivers include:
Water's high specific heat capacity and thermal conductivity enable water cooled condensers to handle massive heat loads efficiently, essential for continuous refinery operations.
Shell-and-tube designs with stainless steel, copper-nickel, or titanium tubes withstand corrosive petrochemical process fluids and high operating pressures.
High heat transfer density means smaller equipment footprint compared to air-cooled systems, critical in space-constrained refinery environments.
Water cooling performance is independent of ambient temperature fluctuations, ensuring stable refrigeration system operation across all seasons and climates.
Manufactured under Class I & II Pressure Vessel licenses, meeting ASME, PED, and GB standards required for petrochemical process equipment.
Integration with cooling towers and closed-loop water circuits minimizes water consumption while maximizing refrigeration system COP (Coefficient of Performance).
Petrochemical refining encompasses an extraordinarily diverse range of thermal management challenges. Water cooled condensers in refrigeration systems are deployed across virtually every major refining process, each with distinct temperature, pressure, fluid compatibility, and reliability requirements.
In atmospheric and vacuum distillation units, water cooled condensers in overhead refrigeration systems condense hydrocarbon vapors, enabling efficient product separation. High-capacity shell-and-tube condensers handle the massive vapor loads from distillation column overheads, recovering naphtha, kerosene, and diesel fractions with precision thermal control.
Fluid Catalytic Cracking units generate significant heat and require robust refrigeration systems with water cooled condensers to manage product stream cooling, wet gas compression interstage cooling, and main fractionator overhead condensation. The ability to handle fouling-prone hydrocarbon streams makes high-quality condenser design critical here.
Recovery of LPG (propane, butane) and light hydrocarbons from refinery gas streams requires deep refrigeration systems operating at sub-zero temperatures. Water cooled condensers serve as the high-stage condensers in cascade refrigeration systems, rejecting heat from propylene or ammonia refrigerant circuits efficiently and reliably.
These high-pressure hydrogen-rich processes require precise cooling of reactor effluents and product streams. Water cooled condensers in the refrigeration systems supporting high-pressure separators must withstand hydrogen embrittlement risks, demanding specialized tube materials and design standards — areas where Qiaoxin's engineering expertise provides significant value.
Production of benzene, toluene, xylene (BTX), and ethylene requires precise temperature control at multiple process stages. Water cooled condensers integrated into refrigeration systems support crystallization, absorption, and distillation processes, where even minor temperature deviations can significantly impact product purity and yield.
LNG facilities represent some of the most demanding applications for water cooled condensers in refrigeration systems. Multi-stage refrigeration trains using propane, ethylene, and methane refrigerants rely on high-performance water cooled condensers at the warm end of the refrigeration cycle to achieve the cryogenic temperatures required for natural gas liquefaction.
The petrochemical industry is undergoing a profound transformation driven by decarbonization mandates, digital transformation, and the shift toward more sustainable production methods. Water cooled condenser technology is evolving in parallel to meet these new demands.
As the industry transitions from HFCs to natural refrigerants (ammonia, CO₂, hydrocarbons) and next-generation HFOs, water cooled condensers must be redesigned to handle different operating pressures, fluid properties, and material compatibility requirements.
Digital twin technology and IoT-enabled sensor networks are being integrated into water cooled condenser systems, enabling real-time performance monitoring, predictive maintenance, and remote optimization of refrigeration system efficiency in petrochemical plants.
Advanced tube geometries — including micro-finned tubes, twisted-tape inserts, and surface-enhanced tube bundles — are being adopted to boost heat transfer coefficients, reduce condenser size, and improve overall refrigeration system energy efficiency.
Modern petrochemical facilities are increasingly integrating water cooled condensers into plant-wide heat integration networks, recovering condenser heat for process heating, absorption cooling, or power generation via organic Rankine cycles (ORC).
Pre-engineered, factory-tested skid-mounted refrigeration systems incorporating water cooled condensers are gaining traction in the petrochemical sector, reducing installation time, improving quality control, and enabling faster commissioning of new refinery units.
Tightening water discharge regulations and cooling water quality standards are driving investment in advanced water treatment systems and closed-loop cooling circuits for water cooled condenser installations in petrochemical facilities worldwide.
company profile
Wuhan Qiaoxin Refrigeration Equipment Co., Ltd. was established in 2003 and is located in Wuhan, Hubei Province — China's major transportation hub connecting nine provinces. The company is a modern enterprise specializing in the research, design, manufacture, and sales of shell-and-tube condensers, evaporators, and other heat-exchange products. In terms of technology, Qiaoxin has consistently maintained a leading position in the domestic market.
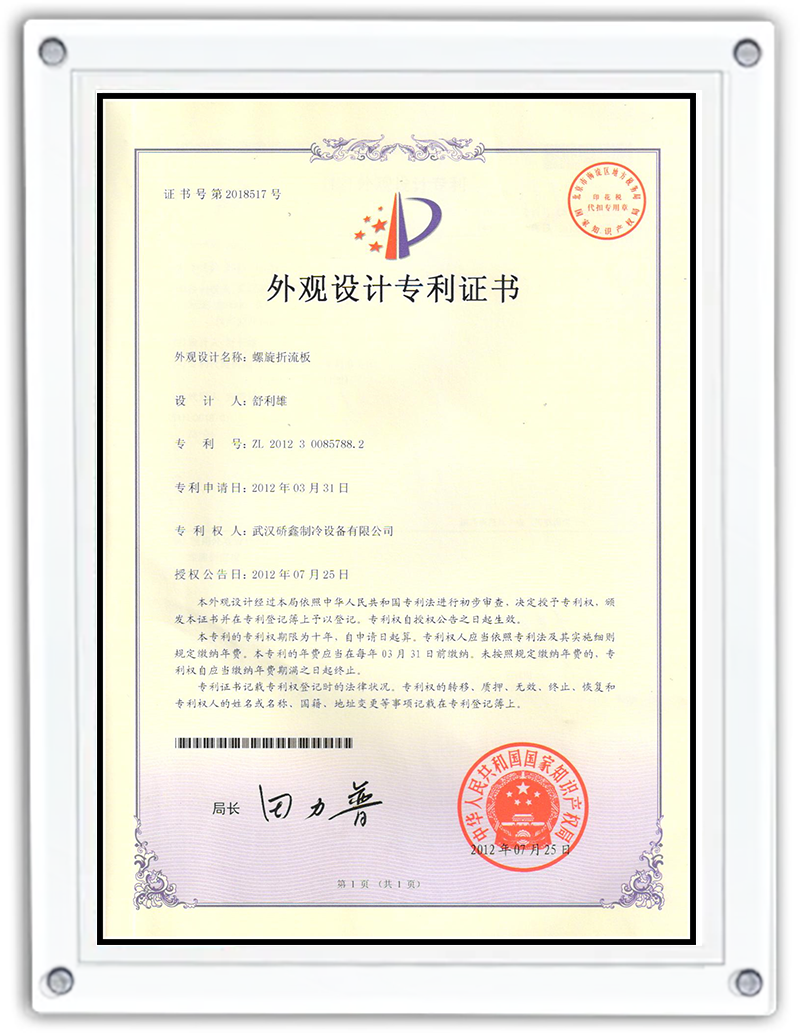
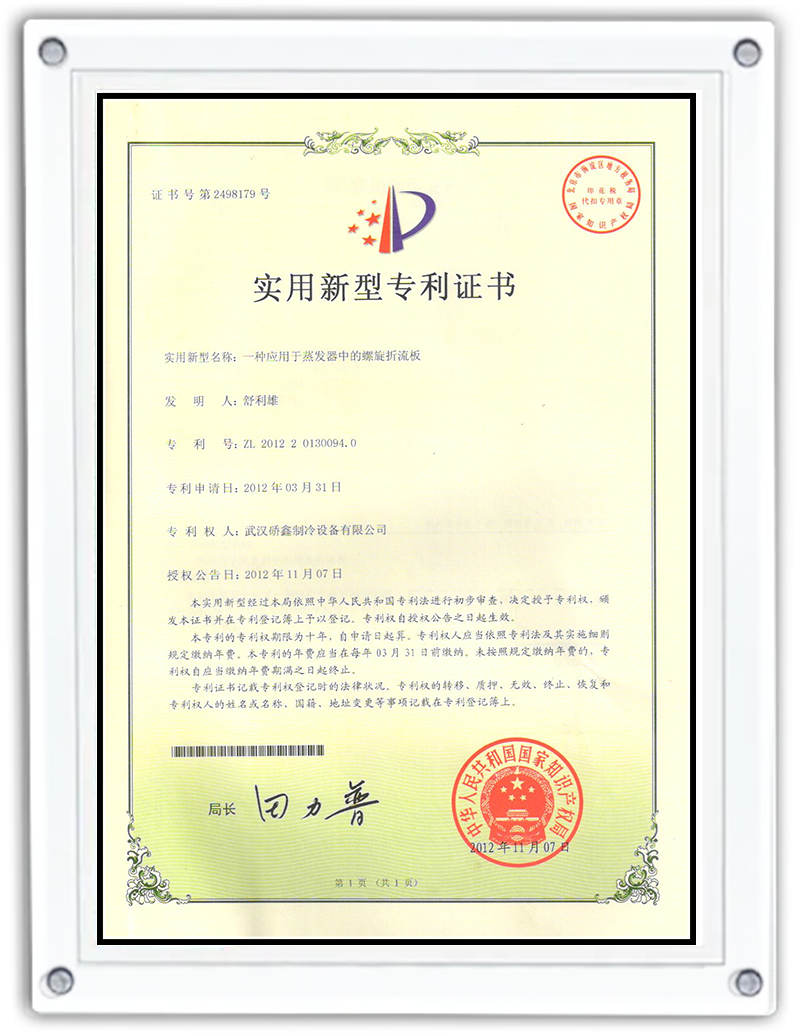
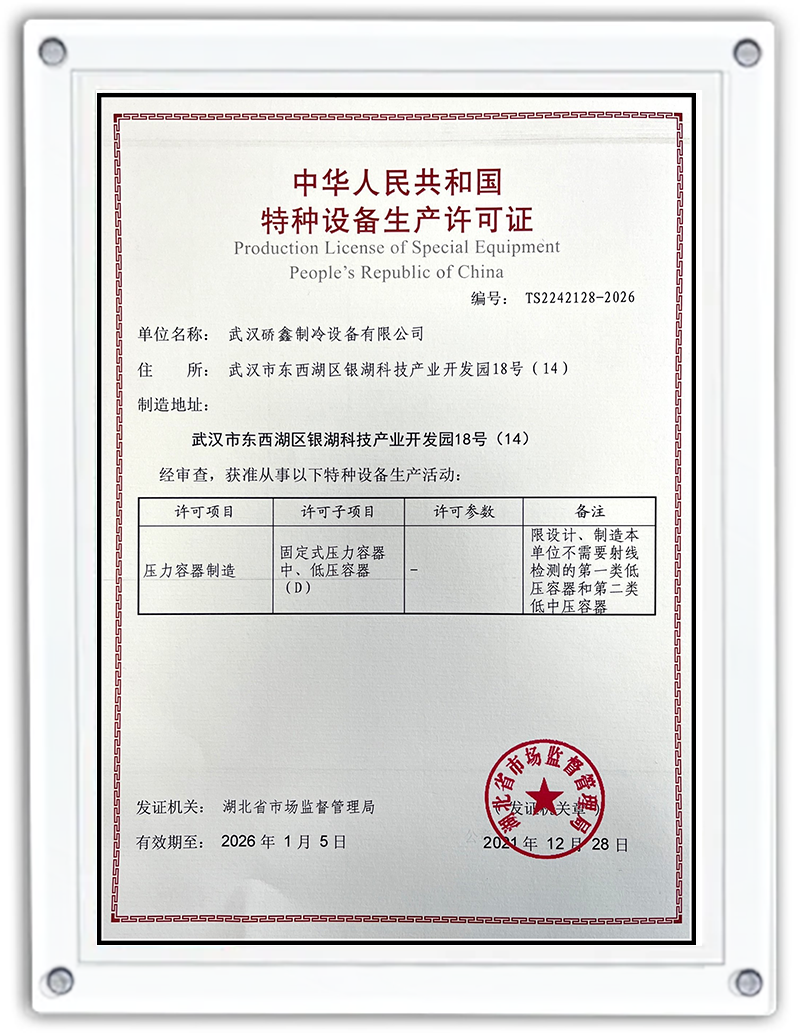
Qiaoxin holds Class I and Class II Pressure Vessel Design Licenses and a Pressure Vessel Manufacturing License. The company is equipped with advanced production facilities, including CNC machining centers, CNC tube expanders, CNC cutting machines, and CO₂ flux-cored gas-shielded welding equipment, as well as a team of experienced professionals who have long been engaged in heat exchanger design and manufacturing. Through continuous research, development, and practical application, Qiaoxin has established a comprehensive management system that encompasses the entire process, from design and manufacturing to installation and commissioning, across a range of heat exchanger types and scales.
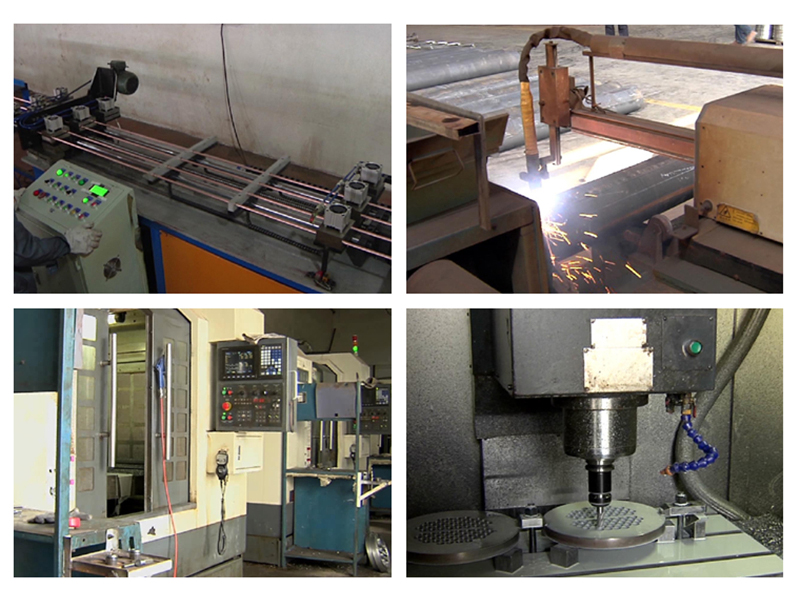
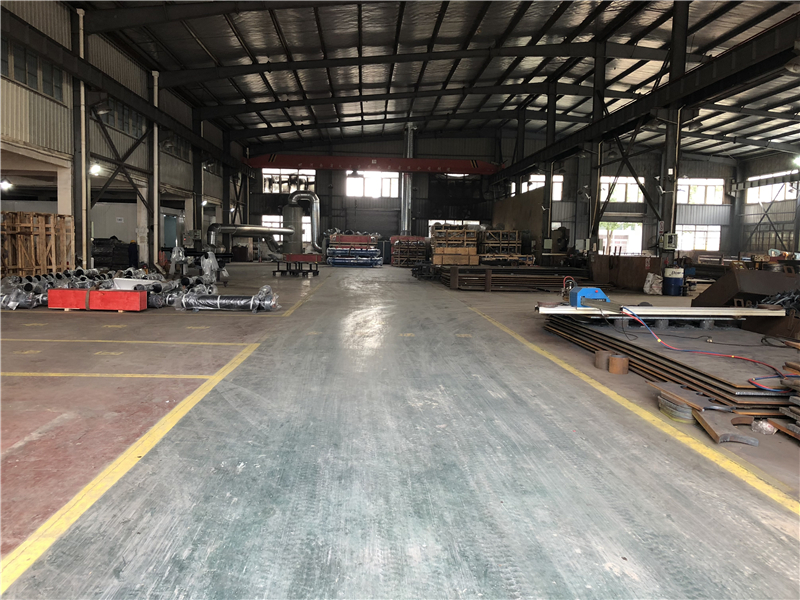
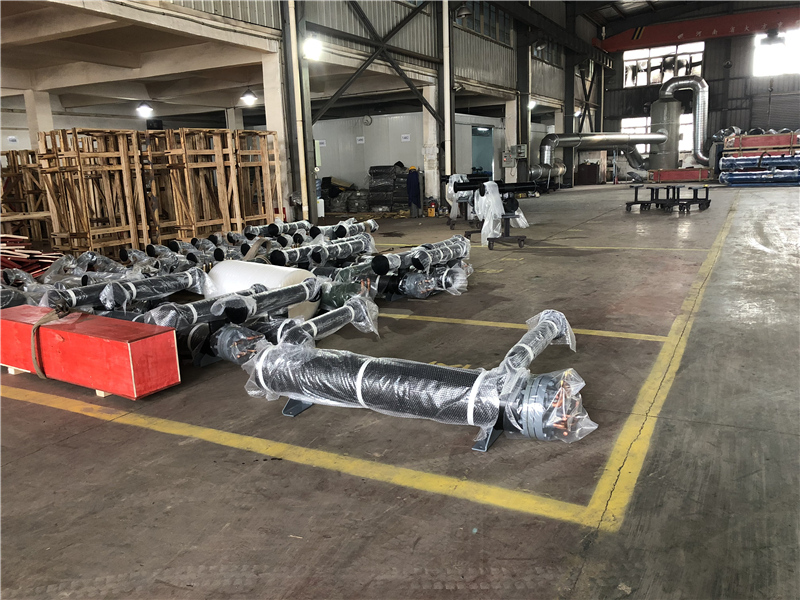
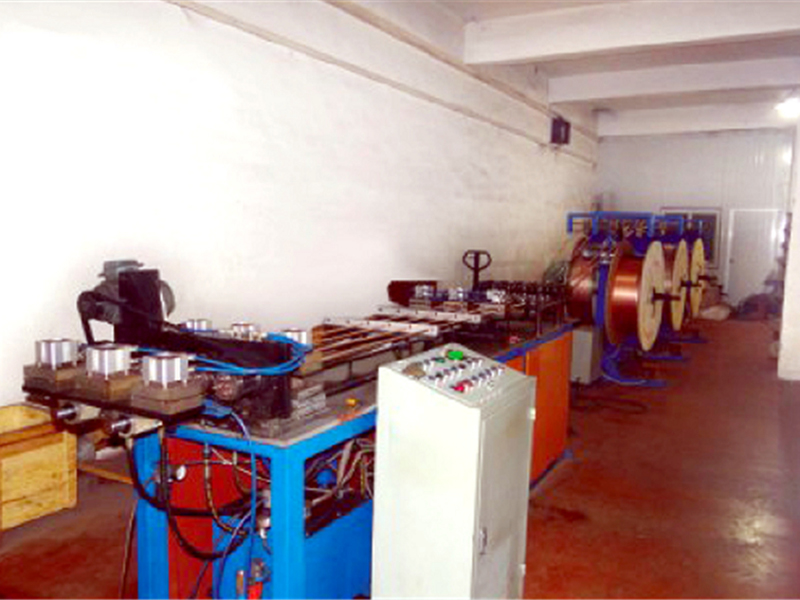
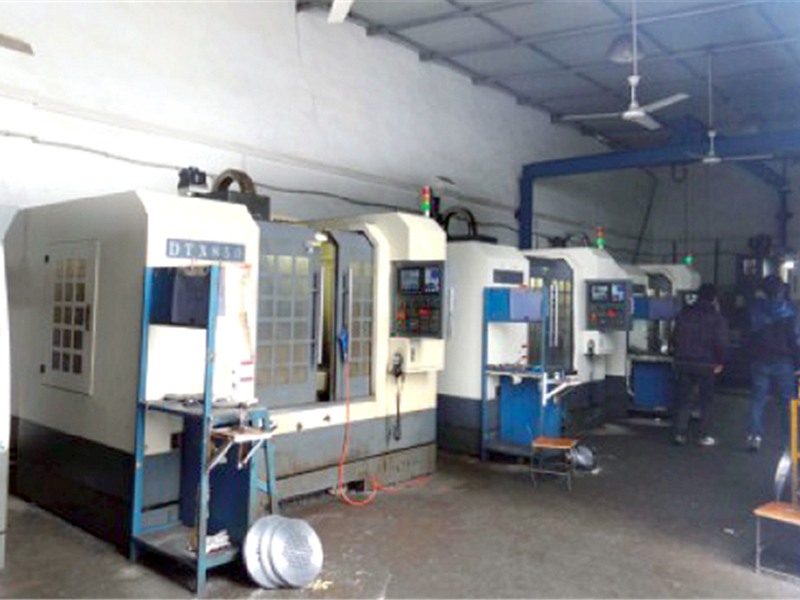
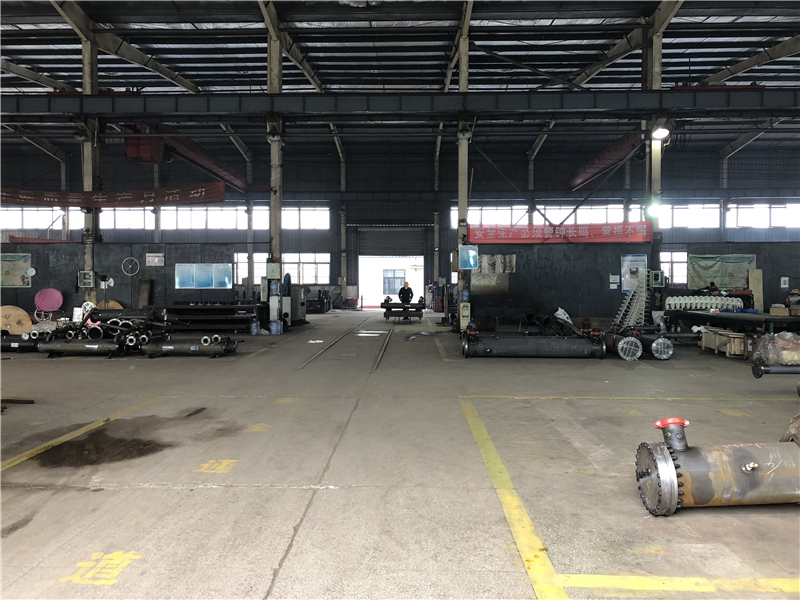
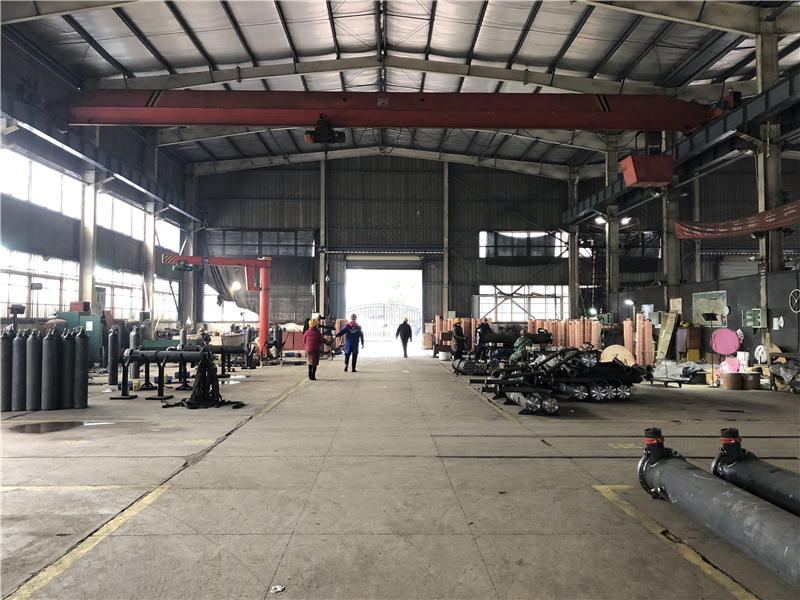
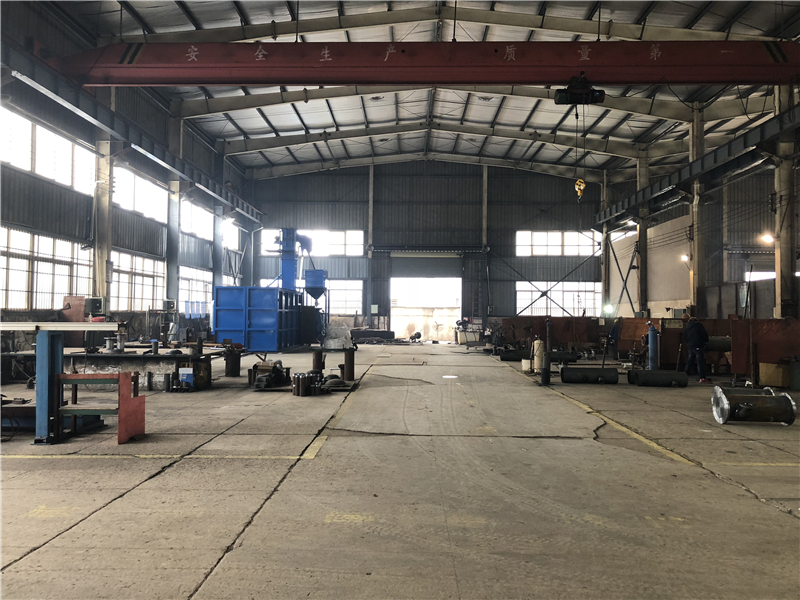
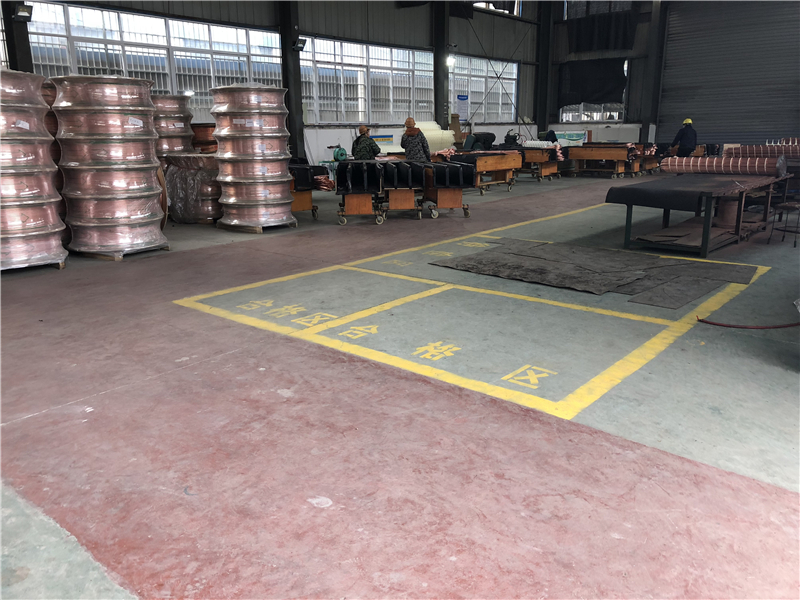
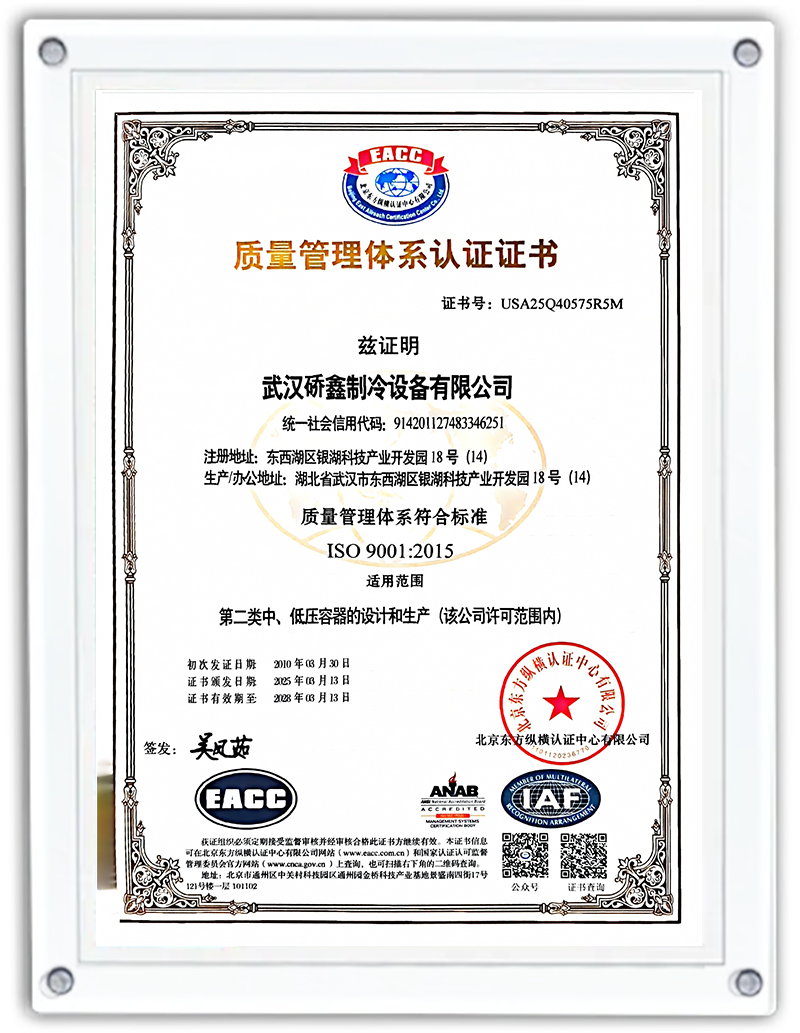
The company is capable of providing products for a wide range of operating conditions, featuring rigorous and innovative designs, meticulous workmanship, and the flexibility to meet diverse customer requirements. Qiaoxin has also passed the ISO 9001:2008 international quality management system certification, ensuring strict control over the entire process of product development, design, production, inspection, and after-sales service through an advanced quality management system.
QiaoXin was established in Wuhan. As a start-up enterprise, the company — like many others — faced challenges in product promotion, financial management, and operational efficiency. Through professional expertise and strong perseverance, QiaoXin successfully overcame these initial obstacles and achieved steady growth.
After only one year of operation, QiaoXin earned the trust of one of China's most well-known enterprises, Midea. This partnership marked a significant milestone, and the two companies have maintained continuous cooperation ever since.
Following four years of rapid development, QiaoXin had built a strong reputation within the domestic market. To support business expansion, the company relocated to its current facility and invested in advanced precision machinery and specialized equipment for heat exchanger manufacturing, further enhancing production capability and product quality.
QiaoXin began supplying products to other internationally recognized corporations, including Dunham-Bush and Carrier. Our products gained broad recognition not only domestically but also overseas, and QiaoXin was increasingly regarded by manufacturers as a reliable and resilient supplier.
QiaoXin officially established its export business, marking a new phase of international development. Since then, our products have been exported to more than 20 countries and regions, including South Korea, Malaysia, Vietnam, and India, among others.
While we are grateful for the achievements made to date, QiaoXin remains committed to continuous improvement and long-term partnership development. We will consistently uphold our core principles by delivering high-quality products at competitive prices. We look forward to the opportunity to serve you and to building a successful and enduring partnership together.
"Quality First, Pursuit of Perfection" is the guiding principle of Qiaoxin's development. After years of growth, the company has earned widespread praise from customers at home and abroad for its outstanding product performance and efficient, responsive service. Its products are exported to Europe and the United States (PED certified), Southeast Asia, Africa, and throughout China, serving well-known domestic air-conditioning brands such as Midea, Chigo, Dunham-Bush, and TICA.
For petrochemical refining clients specifically, Qiaoxin's engineering team provides customized water cooled condenser solutions tailored to the unique process conditions, fluid compositions, pressure ratings, and regulatory requirements of each refinery application. From initial thermal design and material selection through to manufacturing, pressure testing, and on-site commissioning support, Qiaoxin delivers end-to-end expertise that industrial clients can rely on.
Our Mission
Driven by a strong sense of mission toward the advancement of China's refrigeration industry, Qiaoxin is committed to applying cutting-edge refrigeration technologies to promote harmonious coexistence between humanity and nature. Looking ahead, the company will continue to follow a path of harmonious, healthy, and scientifically grounded development, upholding the philosophy that "character comes before products, and quality is the lifeblood of an enterprise." With dedication and enthusiasm, Qiaoxin strives to provide customers with high-value products and reliable, efficient service.
Contact Us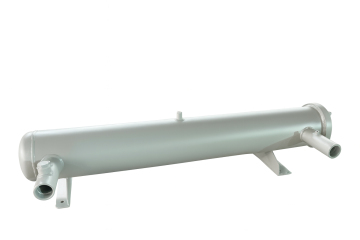 Stainless Steel Water-Cooled Evaporator for Efficient Cooling
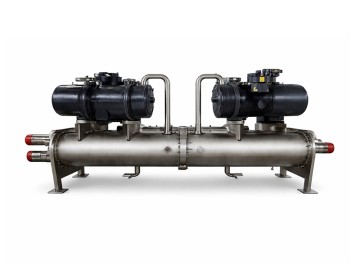 Premium Water Cooling Chiller Unit
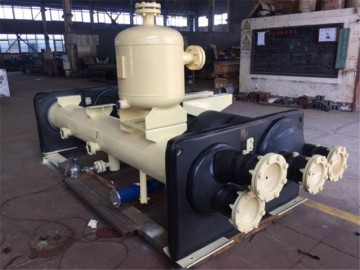 Single-Pass Flooded Evaporator with Condenser and External Oil Separator
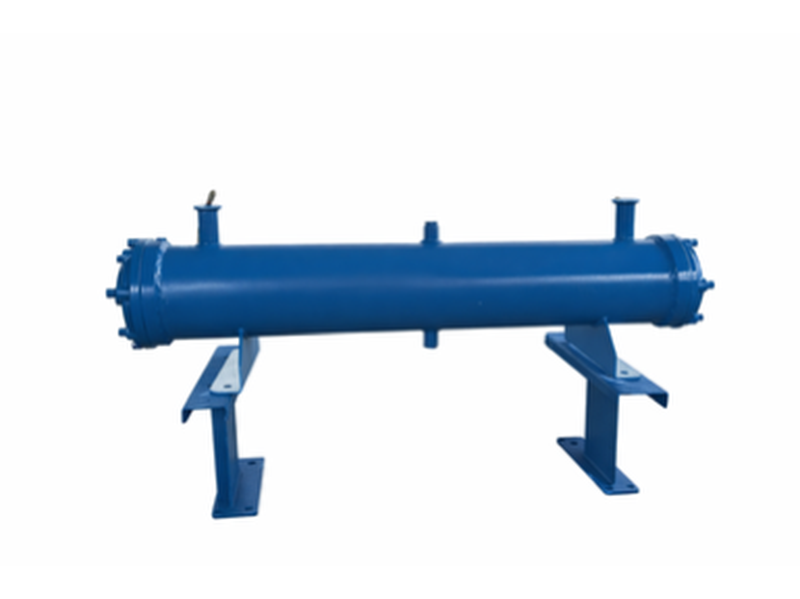 Single-Circuit Condenser
 High-Efficiency Shell and Tube Condenser for Optimal Cooling
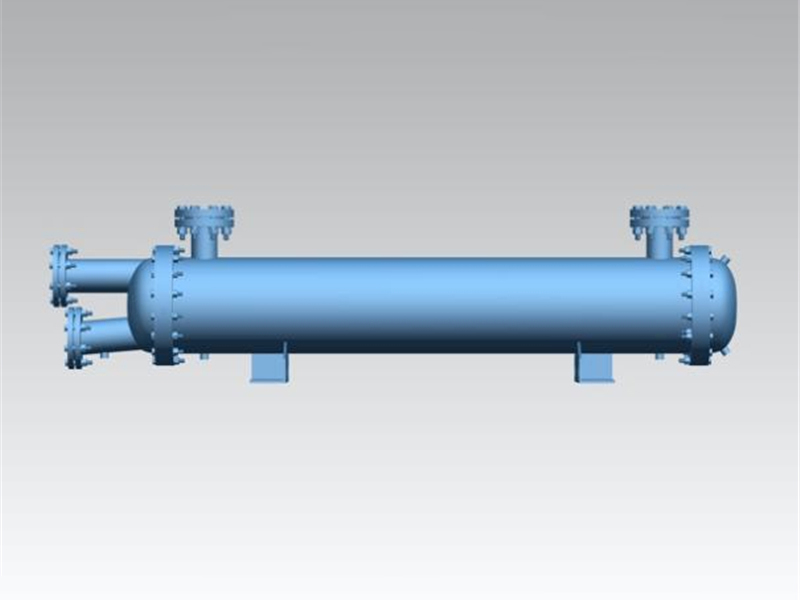 Water-to-Water Heat Exchanger
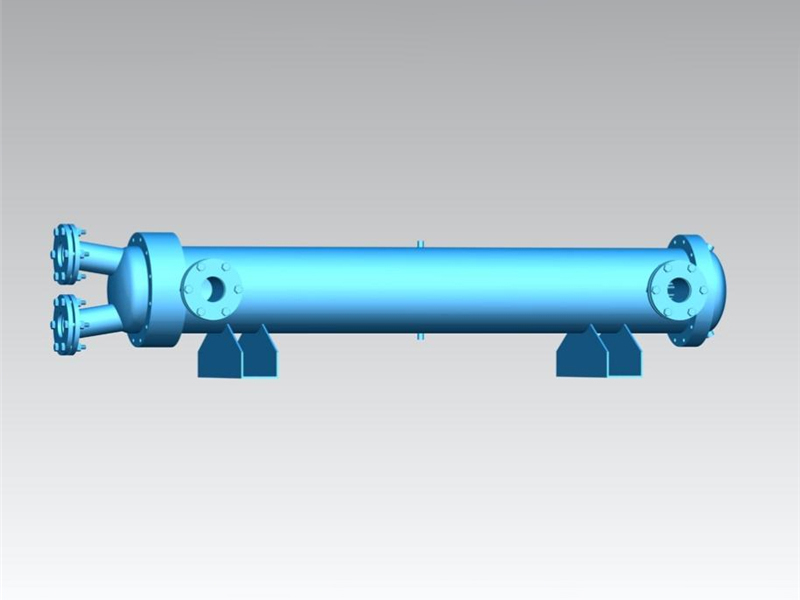 Steam-to-Water Heat Exchanger
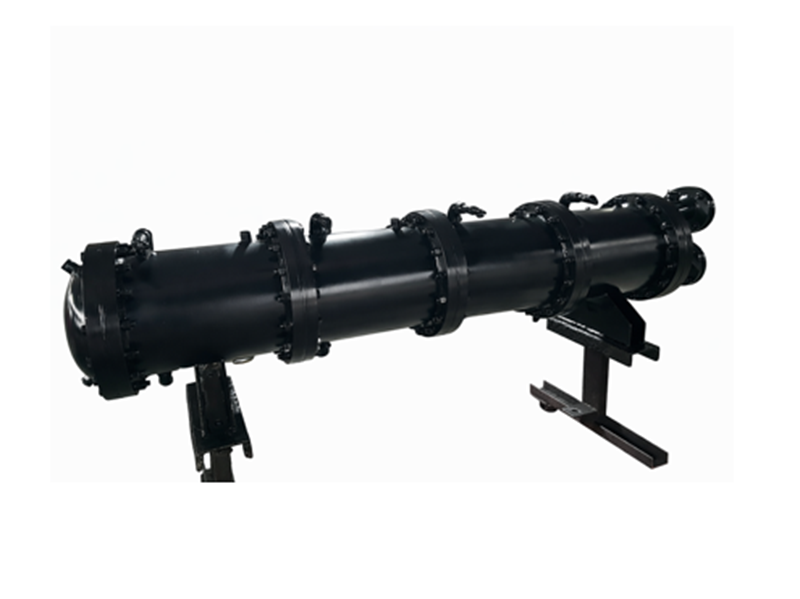 Multi-Circuit Condenser